Choose a pelletizing system by the polymer’s cutting behavior, the required pellet quality and the actual production range. Strand pelletizing cools continuous strands before cutting, water-ring systems cut at the die face before pellets enter the cooling ring, and underwater die-face systems cut inside a water-filled chamber.
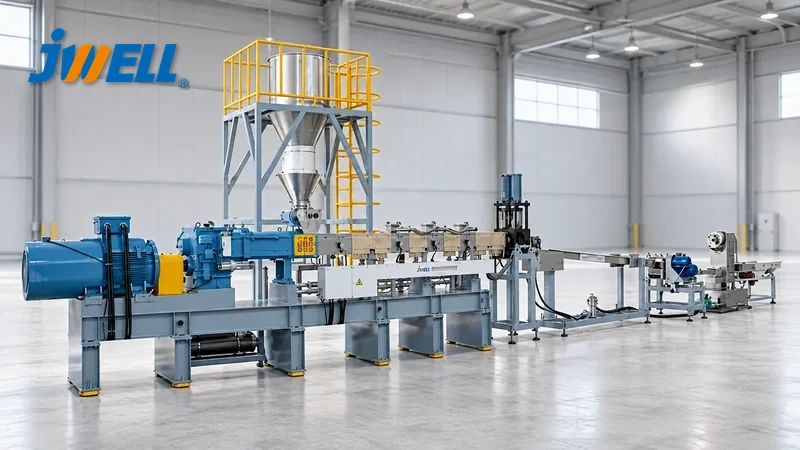
For a straightforward PE or PP recycling project, water-ring cutting is often a useful candidate. Stable, non-sticky strands make conventional strand cutting attractive, especially when operators need easy access during product changes. Underwater die-face cutting merits consideration when the material and production rate justify its die-heating, water-circuit and automation requirements.
Define the cutting mechanism before comparing prices
In conventional strand pelletizing, molten polymer leaves a die as continuous strands. The strands pass through a cooling stage, are dewatered as required and enter a cutter. The resulting pellets are generally cylindrical, with their dimensions influenced by strand size, feed speed and cutting frequency.
In water-ring pelletizing, rotating knives cut emerging melt at the die face. The pellets are thrown outward into a surrounding water ring, which cools and transports them to separation and drying equipment.
In underwater die-face pelletizing, the cutting takes place directly against the die inside a water-filled chamber. Water carries the pellets to separation and drying equipment. Die heating, water conditions and startup sequencing must keep the process stable.
Underwater strand cutting is a further configuration. It handles formed strands and is not equivalent to underwater die-face cutting. Ask suppliers to mark the cutting point on the process diagram whenever a quotation simply says “underwater.”
Compare complete systems
|
Factor |
Conventional strand |
Water-ring |
Underwater die-face |
|---|---|---|---|
|
Cutting location |
After strand cooling |
At die face before ring cooling |
At die face inside water chamber |
|
Typical pellet form |
Cylindrical |
Rounded or lenticular, formulation-dependent |
Often rounded, process-dependent |
|
Main operating concern |
Strand stability and cutter feeding |
Clean cutting and pellet separation |
Die-hole stability and water/cutting control |
|
Cooling equipment |
Bath or other strand cooling arrangement |
Water ring and circulation system |
Chamber and controlled water circuit |
|
Changeover considerations |
Bath, die and cutter cleaning |
Die, knives, ring and dryer cleaning |
Die, chamber, water system and dryer cleaning |
|
Selection evidence |
Continuous strands and acceptable cut |
Stable hot cutting without agglomeration |
Stable cutting across the agreed output range |
Automation levels vary within each family. Automatic strand threading can change the labor comparison, while an underwater system with poor startup control can lose output despite high installed capacity.
Start with the polymer and formulation
Conventional strands are useful when the melt forms stable strands that survive cooling and feeding. Frequent breaks can increase waste and operator attention. Causes can include formulation changes, contamination, unstable extrusion, die conditions or inadequate cooling.
Water-ring systems are common candidates for suitable PE and PP recycling applications. However, low melt viscosity, tackiness or particular fillers can change cutting and cooling behavior. Do not extend a successful trial on one polyolefin grade to every formulation.
PET needs a different starting point from typical PE or PP recycling. Water-ring cutting is often a poor fit for PET; strand systems are the more common route unless a die-face design is proven for that grade. Evaluate conventional strand, underwater strand or a specifically engineered underwater die-face system for PET; a water-ring proposal needs material-specific operating evidence.
Underwater die-face systems can process a broad range of formulations when configured correctly. Nevertheless, sticky materials, abrasive fillers and low-rate operation can create different design requirements. Request evidence for the intended formulation instead of assuming a broad material list establishes stable production.
JWELL’s PET bottle flakes recycling pelletizing machine is offered with conventional water-cooled strand and water-immersed strand arrangements. The machine pictured below supports the strand discussion; it is not an illustration of an underwater die-face cutter.
<!–WPIMG:0–>
Evaluate operating range and pellet dimensions together
The pelletizer must match the upstream extruder’s real range. A system sized only for maximum output may perform poorly during small orders or reduced-rate production. Minimum stable throughput matters when formulation development or frequent changes are part of the business.
For strand cutting, pellet length relates to strand feed speed and effective cutting frequency. Strand diameter depends on melt flow through the holes, draw and cooling. The combined setup determines the pellet dimensions and their consistency.
For die-face systems, throughput per hole, knife speed, polymer behavior and cooling affect pellet size and shape. At fixed throughput and die-hole count, increasing knife speed generally reduces pellet mass, but excessive speed or poor blade contact can create fines and accelerate wear.
Agree the customer’s pellet requirements: size distribution, oversize fraction, fines, bulk density, moisture and feeding behavior. A visually round pellet may offer little value if it fails the customer’s drying or dosing requirements.
Include water treatment and drying
All water-contact routes require a defined water balance. Separate circulation flow from fresh-water makeup and heat removal. Confirm filtration, operating temperature, heat exchanger duty and the treatment of solids carried into the water circuit.
A centrifugal dryer removes surface water. Hygroscopic polymers such as PET may still need desiccant drying before their next melt-processing step. Establish pellet moisture at packaging and again at the point of use, especially after storage or transport.
Compare complete equipment boundaries. A pelletizer quotation without the dryer, water skid, heat exchanger or control interfaces may look inexpensive while shifting significant cost to the buyer.
Define pellet temperature at collection and storage conditions. Warm pellets can agglomerate, while moisture uptake during storage can change their readiness for the next process. Include the transfer and packaging system in the trial discussion.
Compare cost per accepted kilogram
Strand systems can offer accessible inspection and a straightforward process, but labor, strand breaks and changeovers affect the result. Water-ring and underwater systems bring their own die, knife, water and drying maintenance requirements. Compare quotations after aligning the scope and automation level.
Use:
Specific electricity consumption (kWh/kg) = measured electricity used within the agreed system boundary ÷ accepted pellet mass.
For an illustrative run consuming 120 kWh and producing 600 kg of accepted pellets, the result is 0.20 kWh/kg. This is a calculation example, not a performance claim for any cutting method. State whether extrusion, water cooling, drying and conveying are included.
Also count startup loss, off-spec pellets, knife and die wear, cleaning time and operator attendance. Maintenance access and spare-part availability can affect operating economics as much as a small difference in rated drive power.
<!–WPIMG:1–>
Require a representative material trial
Test the actual feedstock or compound, including its normal variation in moisture, filler and contamination. Run the intended low and high production rates. Record extrusion stability so upstream disturbances are not incorrectly attributed entirely to the cutter.
Measure accepted pellet mass, dimensions, fines, agglomerates and moisture over an agreed period. Include a planned stop and restart where appropriate, and record waste and recovery time. Retain samples for the customer’s feeding or conversion trial.
Include startup sequencing, cleaning and knife replacement in operator training. Treat strand and underwater die-face cutting as different equipment families in the purchase specification: identify the cutting point, cooling circuit, dryer and controls in the quoted scope.
FAQ
Is underwater strand pelletizing the same as underwater die-face pelletizing?
No. Underwater strand systems cut formed strands; underwater die-face systems cut directly at the submerged die. Their mechanisms and operating requirements differ.
Is water-ring pelletizing suitable for PET?
Do not assume so. Obtain supplier evidence for the exact system and PET grade. Conventional or underwater strand routes and properly configured underwater die-face systems are distinct alternatives to evaluate.
Which system produces the best pellets?
The answer depends on the customer’s specification. Compare size distribution, moisture, fines and feeding performance using the intended material.
Which system uses the least labor?
Compare actual automation and trial attendance. Automatic strand handling, startup behavior and cleaning frequency can change the result substantially.
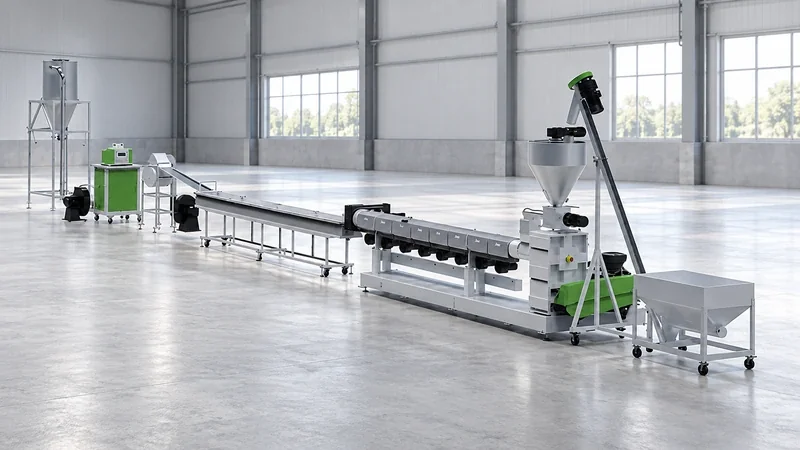
Request a Quote for a JWELL Recycling Pelletizing Line
Purchase a JWELL pelletizing line configured for your polymer and finished-pellet requirements. For PET flakes, ask about JWELL’s strand and water-immersed strand configurations; for other suitable recycling feedstocks, request a single-screw pelletizing line with the appropriate filtration and downstream cutting package.
Send your resin, melt-flow or IV data, filler content, feed moisture, output range and required pellet size to JWELL Anhui sales. Request an equipment quotation covering feeding, extrusion, filtration, cutting, water handling and drying. Have the offer name the cutting method explicitly, including whether any proposed underwater equipment cuts strands or cuts at the die face.