

jwell News
2026-09-22
How to Reduce Material Waste in Plastic Pipe Production
The most effective way to reduce waste in plastic pipe extrusion is to control the process before scrap is created. Learn how feeding, melt pressure, startup, cooling, dimensional inspection, changeovers,...
2026-09-22
Plastic Sheet Extrusion Troubleshooting: How to Eliminate Periodic Transverse Lines
Periodic transverse lines on extruded sheet usually come from one of three zones: the calender drive, the speed and pressure relationship between the die and haul-off, or excessive die shear....
2026-09-22
Which Waste Materials Have Higher Pelletizing Value
Clean, single-polymer waste usually produces the most valuable pellets. This guide compares PET bottles, HDPE and PP rigid scrap, PE films, woven bags, and mixed waste by purity, preparation cost,...
2026-09-12
How Much Factory Space, Power and Labor Does an Extrusion Line Need?
Before ordering an extrusion line, plan more than the machine footprint. This guide provides practical planning ranges for factory space, installed power, cooling water, compressed air, maintenance access and operators...
2026-09-08
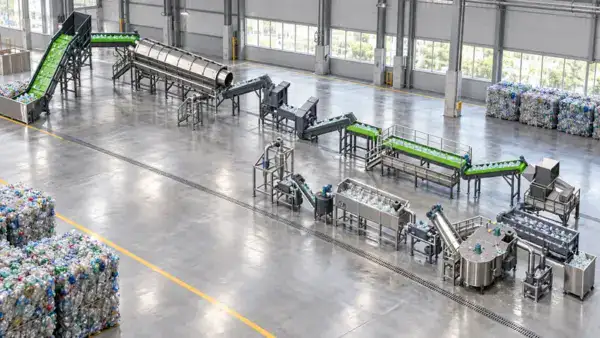
PET Bottle Washing and Pelletizing Line: Complete Process Explained
A PET bottle washing and pelletizing line combines sorting, crushing, hot and cold washing, rinsing, drying, extrusion, melt filtration and pelletizing. Learn how each stage affects PET purity, moisture, intrinsic...
2026-09-02
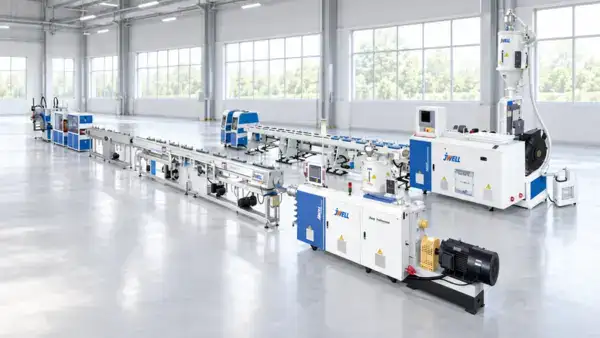
How to Select Extrusion Line Capacity: 300, 500 or 1,000 kg/h
Choosing between a 300, 500 or 1,000 kg/h plastic extrusion line depends on saleable demand, utilization, product mix and future growth—not simply the largest nameplate. This guide explains how to...
2026-08-24
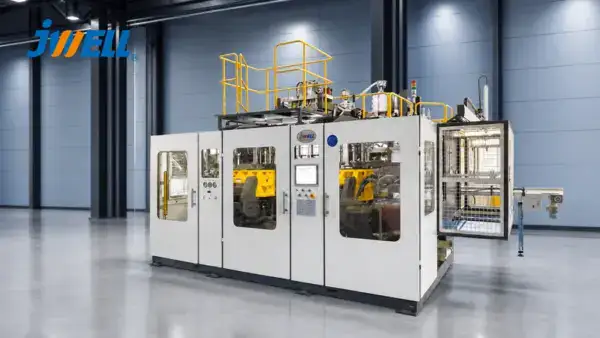
All-Electric vs Hydraulic Extrusion Blow Molding Machines
Choose an all-electric extrusion blow molding machine for clean production, repeatable motion, low idle-energy use and precise small-to-medium packaging. Hydraulic or hybrid systems are often preferred when high clamp force,...
2026-08-24
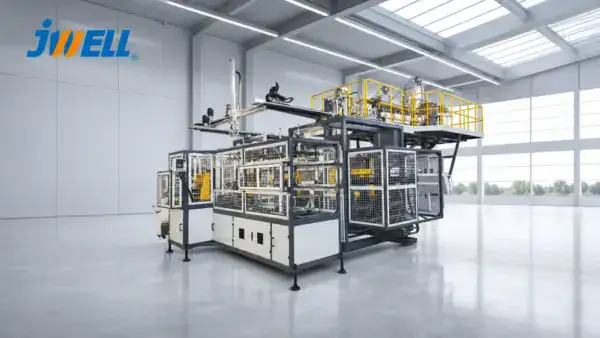
How to Control Parison Sag in HDPE Blow Molding
Reduce parison sag by using an HDPE grade with adequate melt strength, controlling actual melt temperature, shortening unsupported hanging time and programming extra wall thickness where drawdown is greatest. For...
2026-08-17
Medical-Grade PVC Pelletizing: Process and Machine Control
Reliable PVC pelletizing for medical applications requires a locked formulation, qualified raw materials, controlled mixing, low thermal history, contamination prevention and lot-level release testing. The pelletizing machine cannot make a...
2026-08-10
TPU/ABS Automotive Interior Lamination: In-Mold vs Adhesive
Use integrated adhesive-free TPU/ABS lamination for high-volume automotive sheet when the construction is stable and removing a separate coating, curing and lamination step provides a clear cost or emissions-control benefit....
2026-08-03
Extruder Screw and Barrel Wear: When to Replace Them
Replace or rebuild an extruder screw and barrel when measured wear exceeds the manufacturer's allowable clearance or when confirmed wear prevents the line from meeting output and quality targets within...
2026-07-24
PVC Profile Extrusion Line: Complete Buyer’s Guide
A PVC profile extrusion line is a long-term production system, not simply an extruder with a die. The wrong configuration can create unstable dimensions, weak weld corners, excessive scrap or...